Case Study New South Wales PFAS Remediation Plant – Onterris
Project Highlights
High filtrate quality
Filtrate turbidity of 0.076–0.078 NTU
Efficient, conservative design
TMP of 29 kPa at full design flow, with a conservative 57 LMH flux design
Continuous operation
Recovery above 94%, with 50% redundancy for continuous operation
More about this project
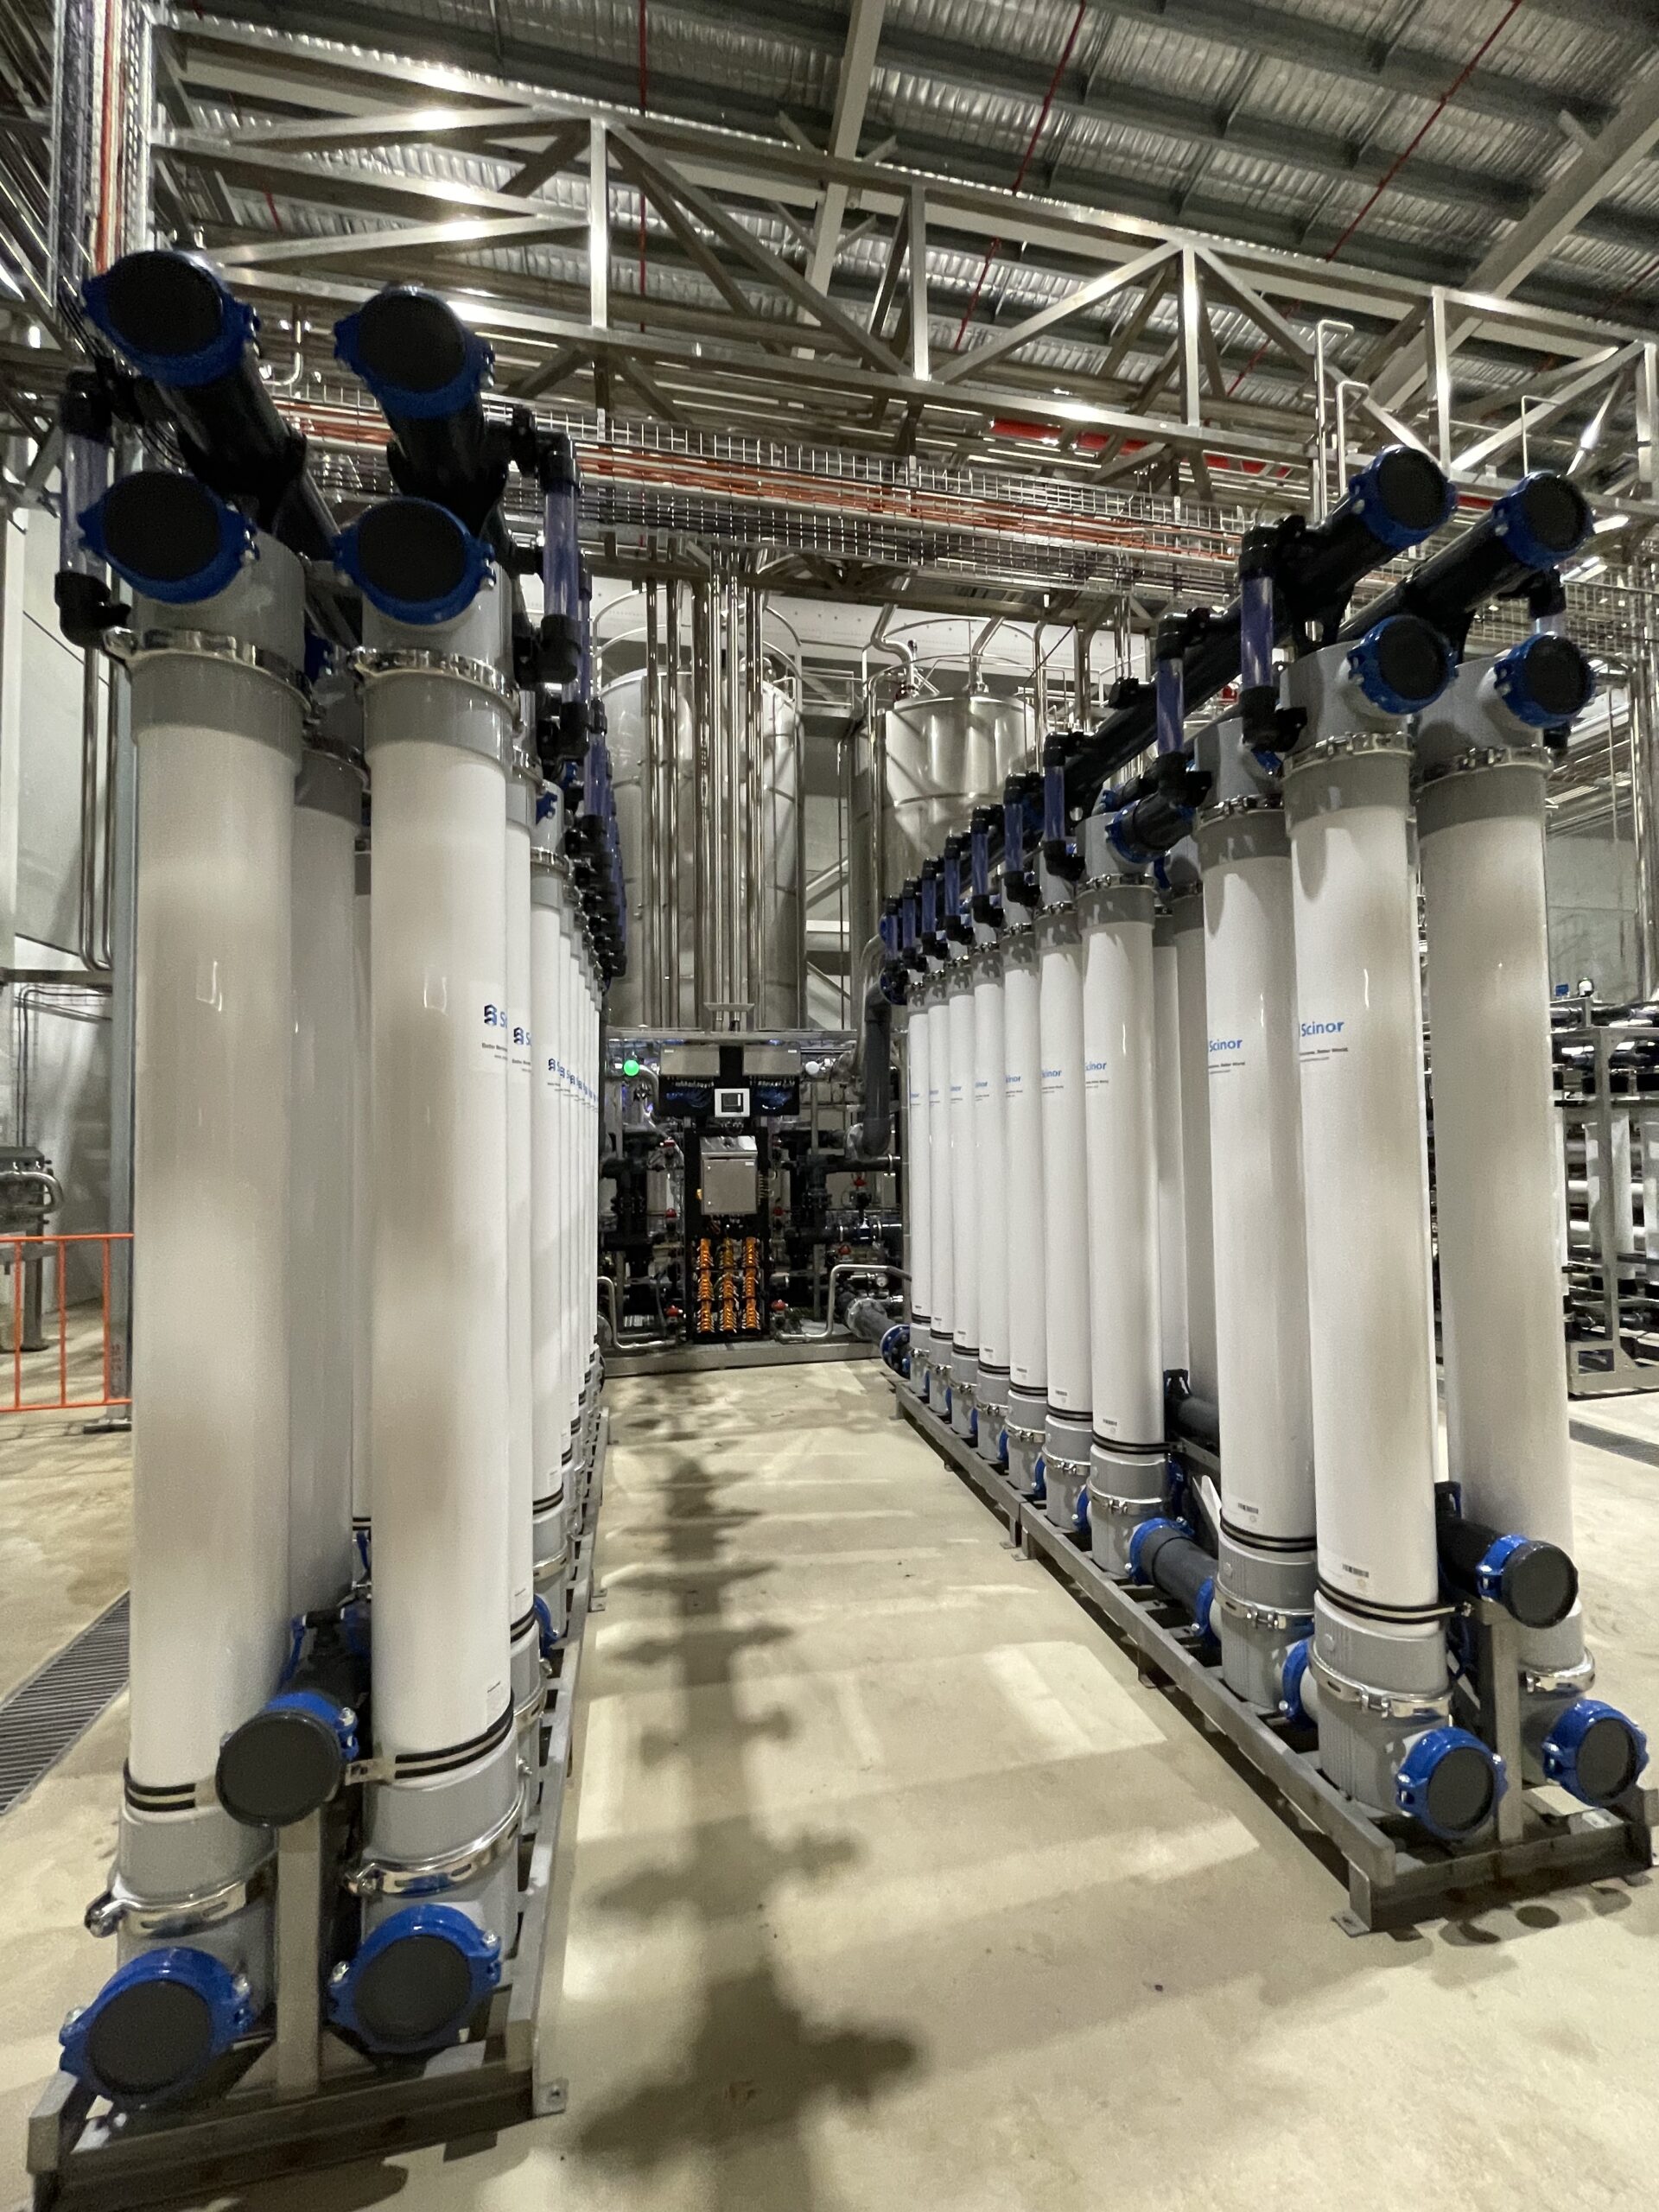
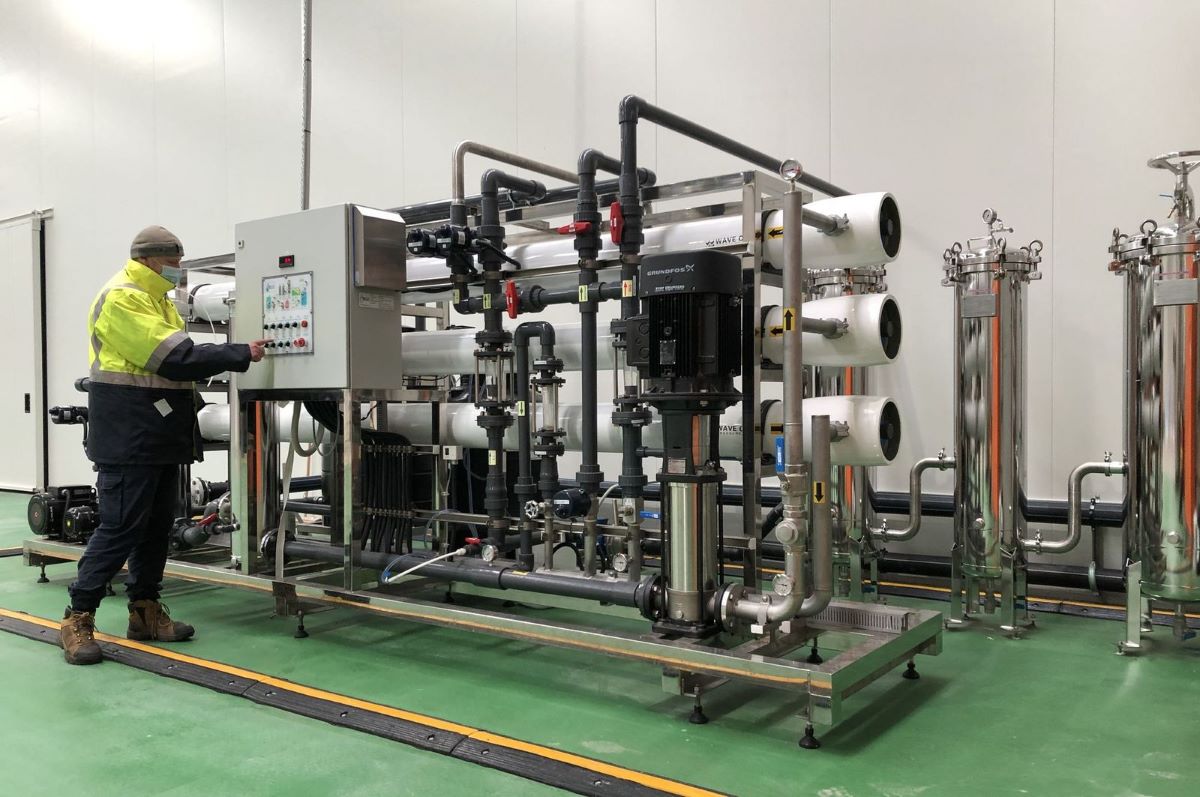
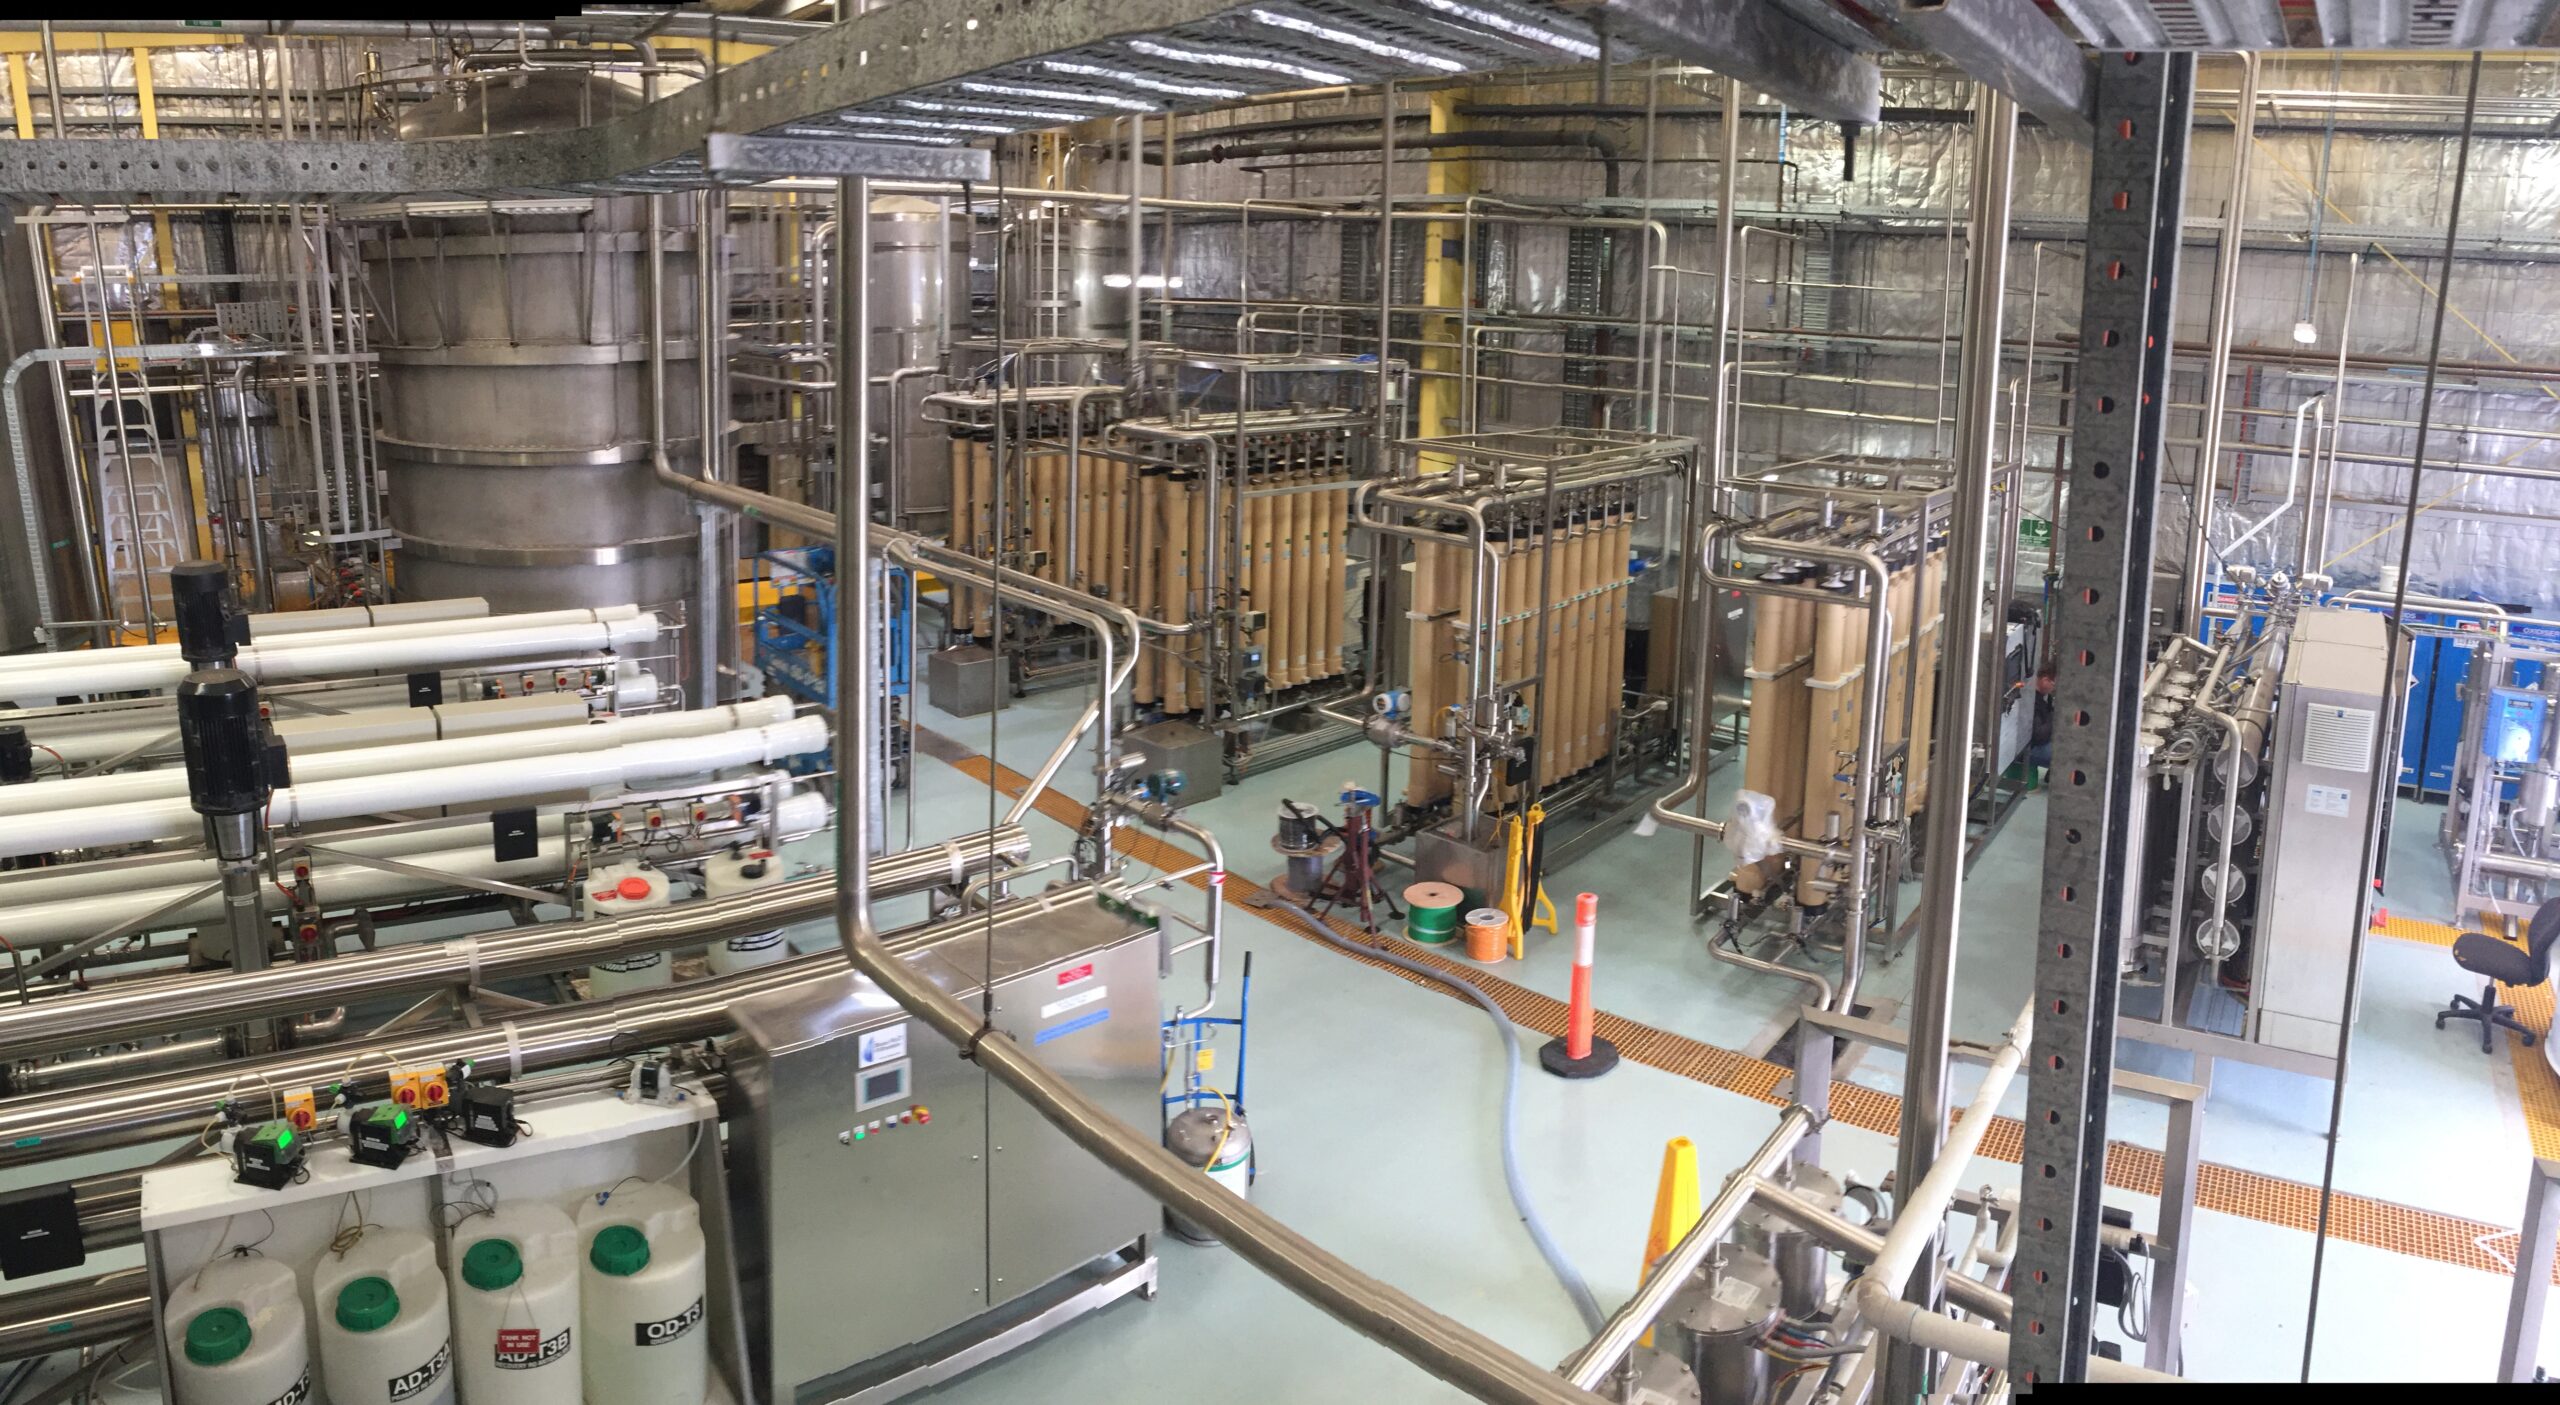
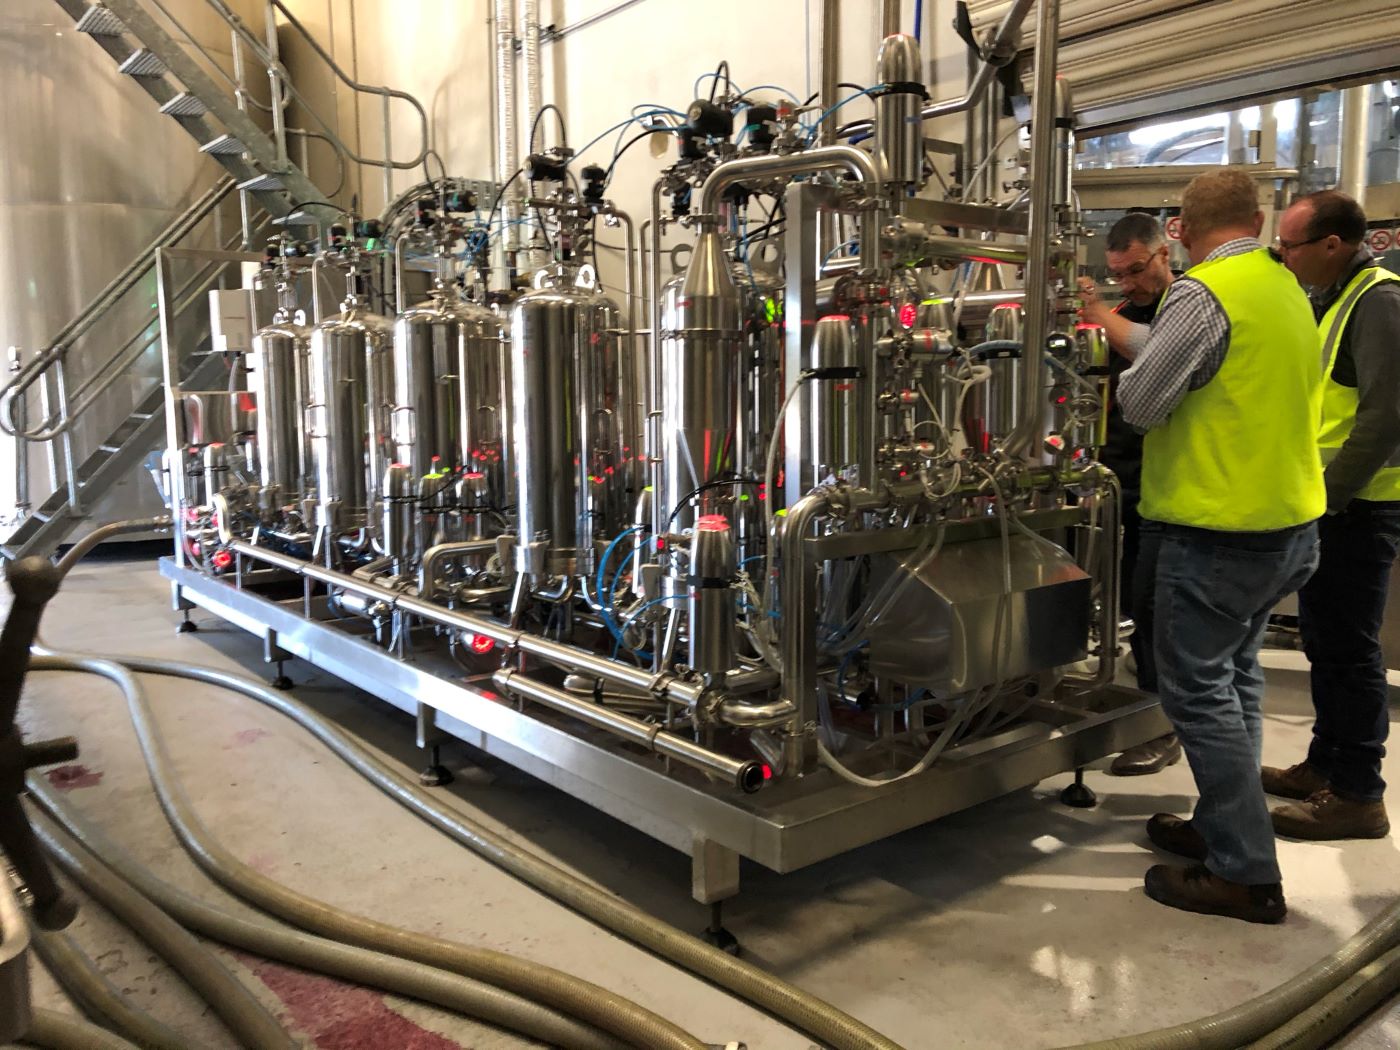
Onterris (formerly ECT2) is a specialist water treatment engineering firm based in Heatherbrae, NSW. Onterris designs, delivers and operates treatment systems for the removal of emerging contaminants, including PFAS, from groundwater, drinking water, landfill leachate and industrial water sources. For this project, Onterris needed an Ultrafiltration system as part of a pretreatment augmentation and capacity upgrade project at one of its PFAS ion-exchange plants at a large client site in NSW.
BHF responded with a fully engineered, factory-tested UF package built specifically around Onterris’ redundancy and integration requirements:
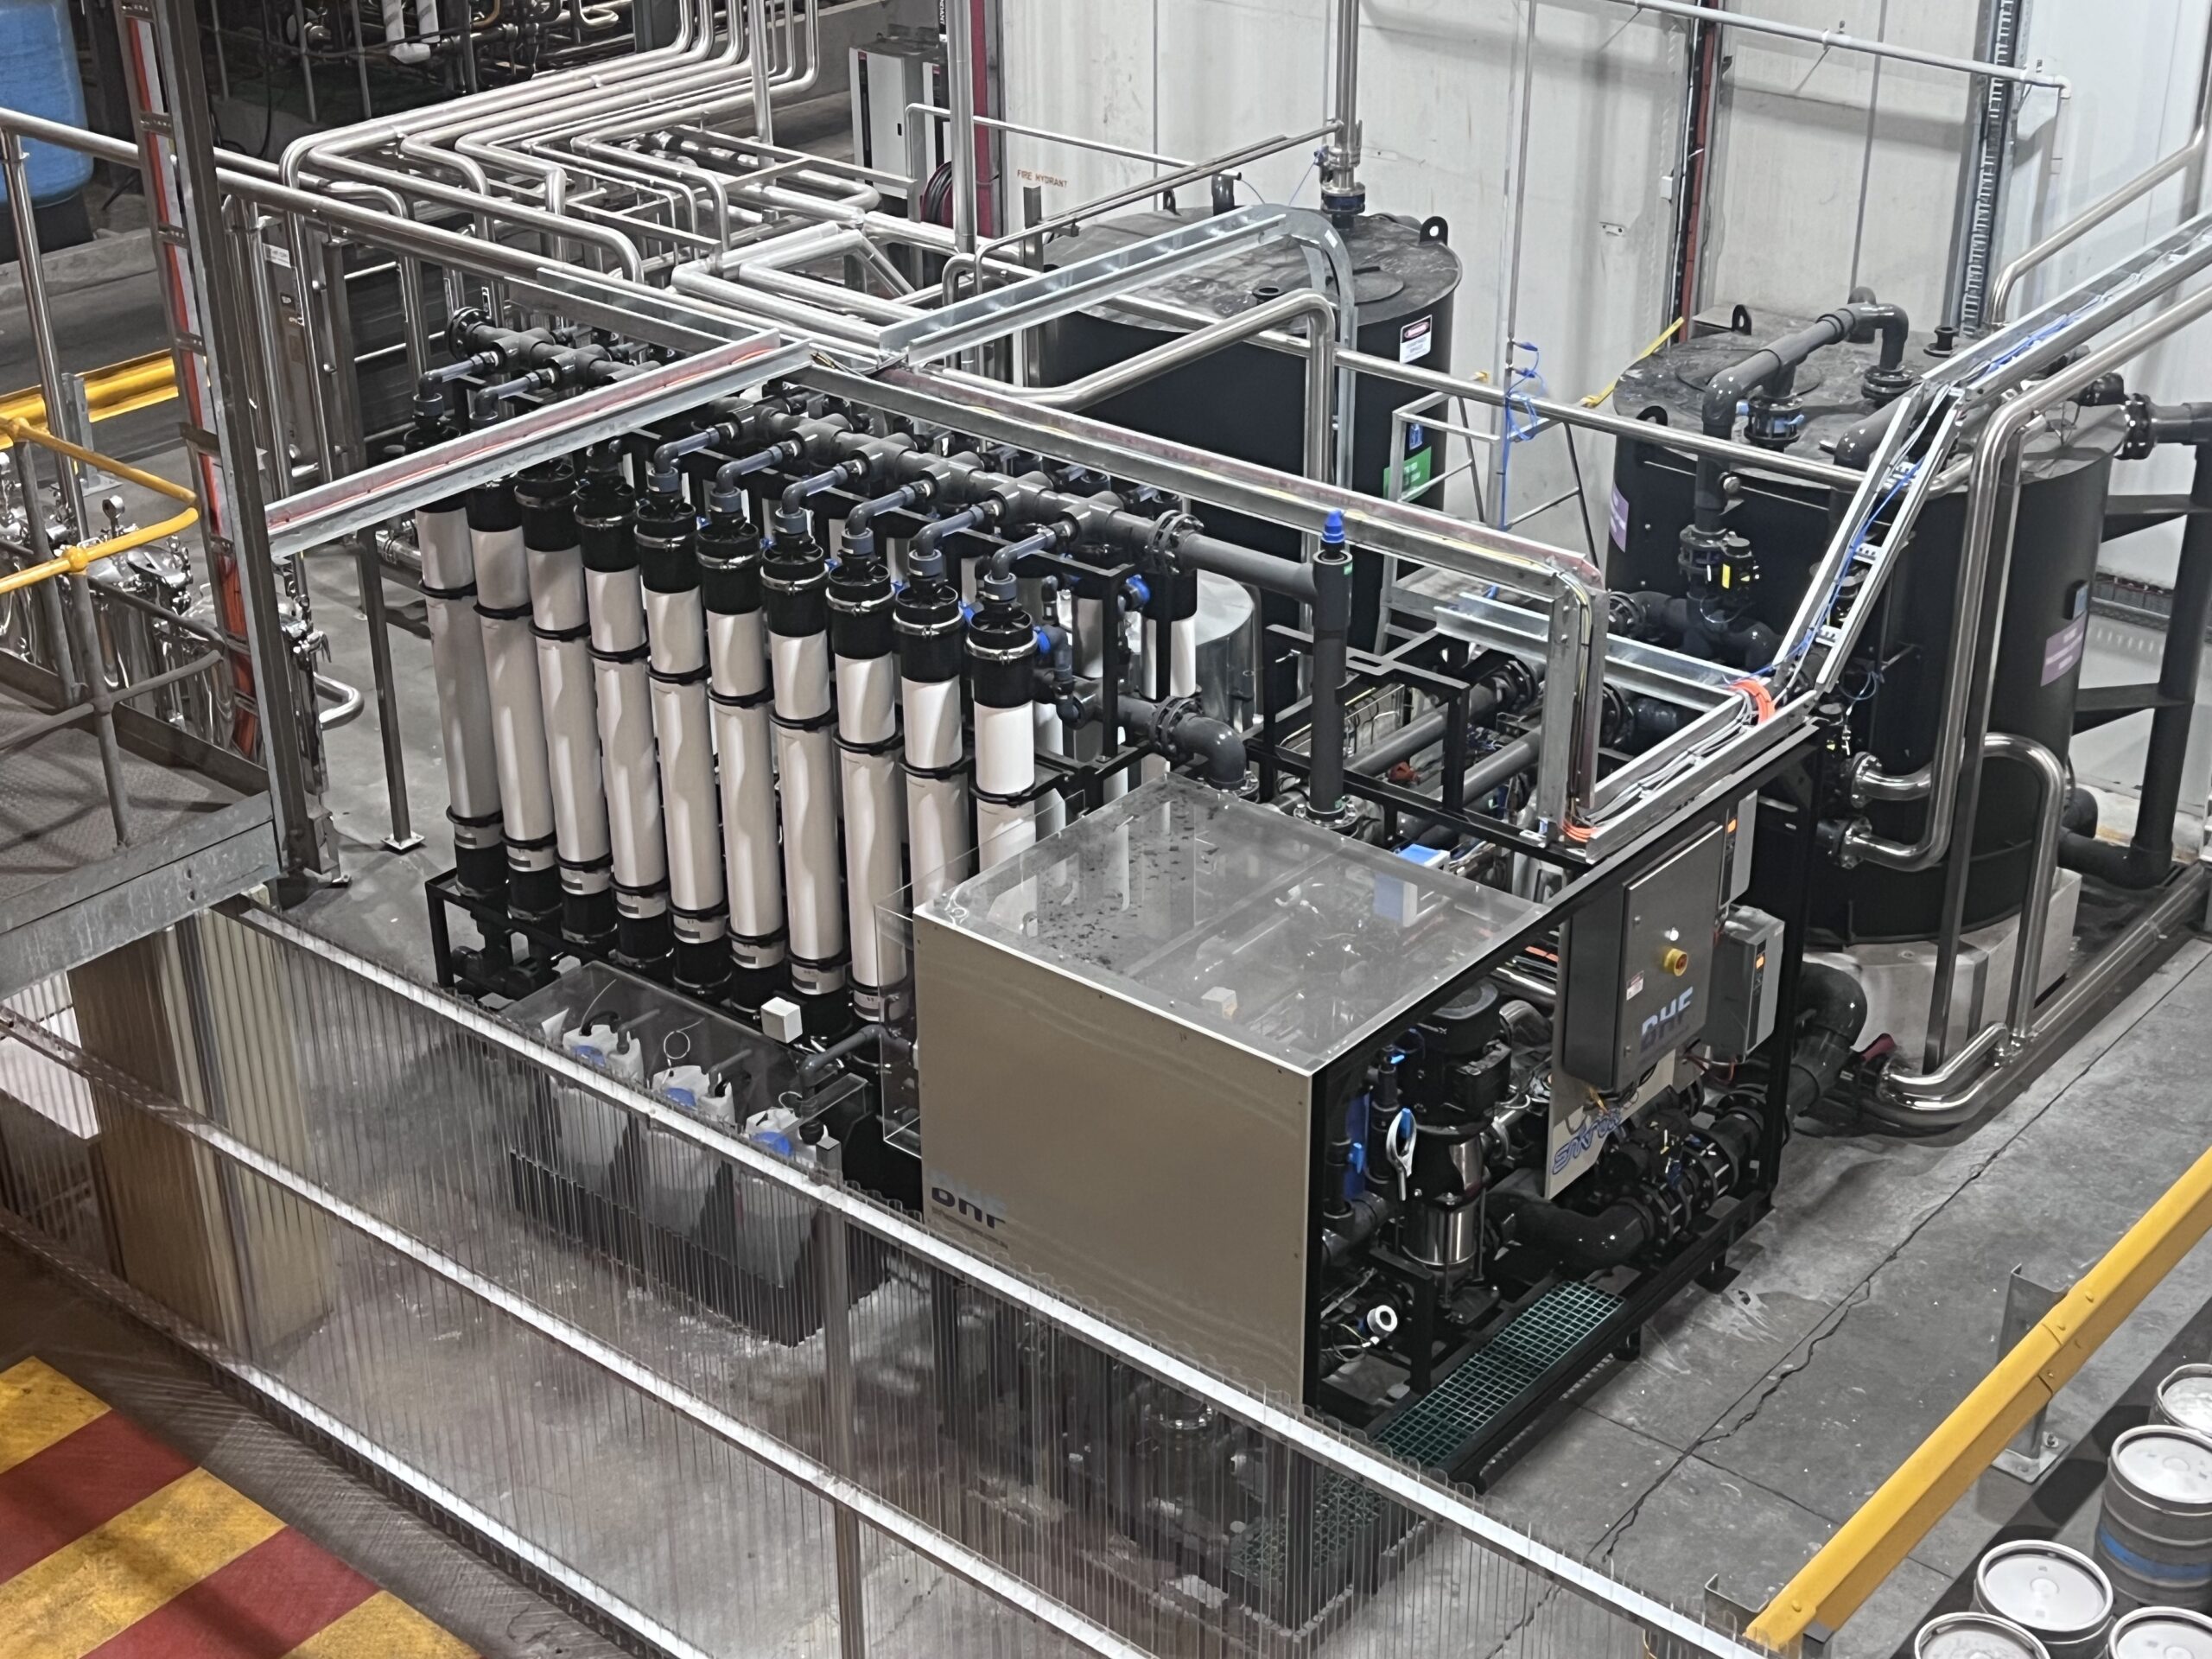
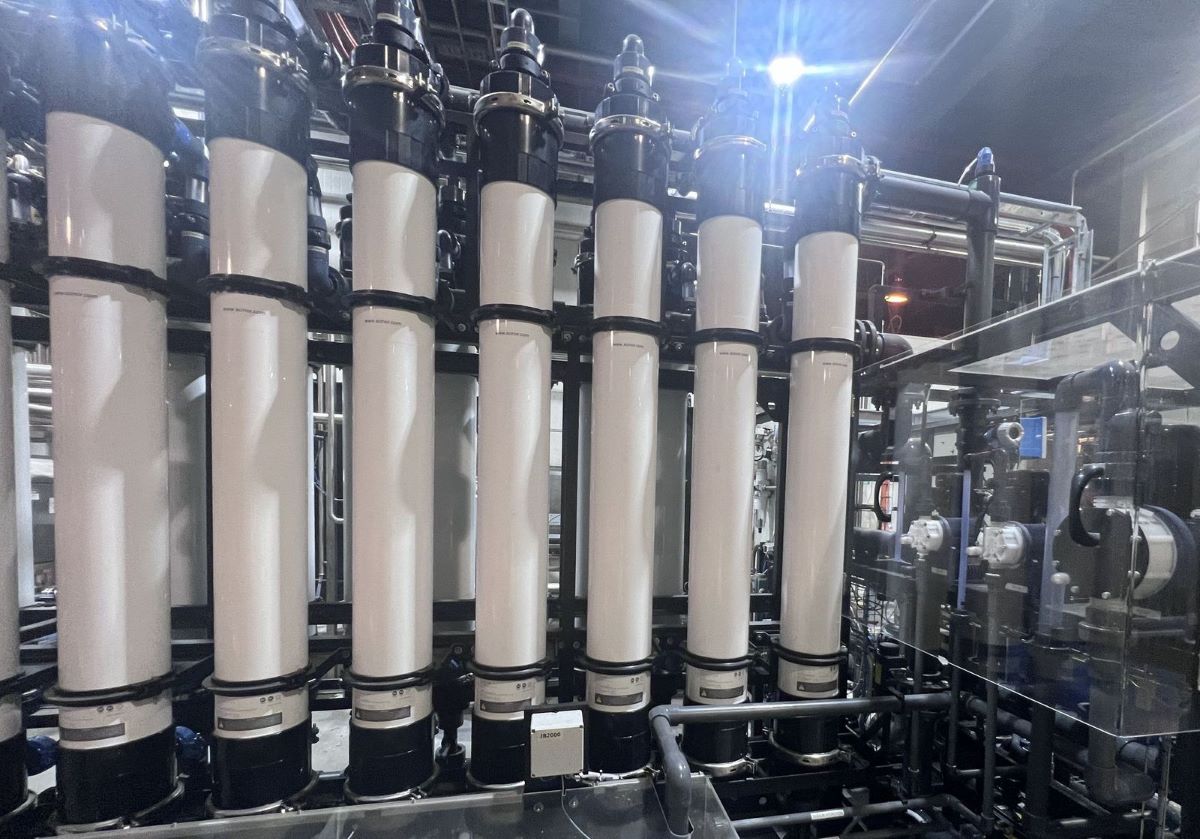
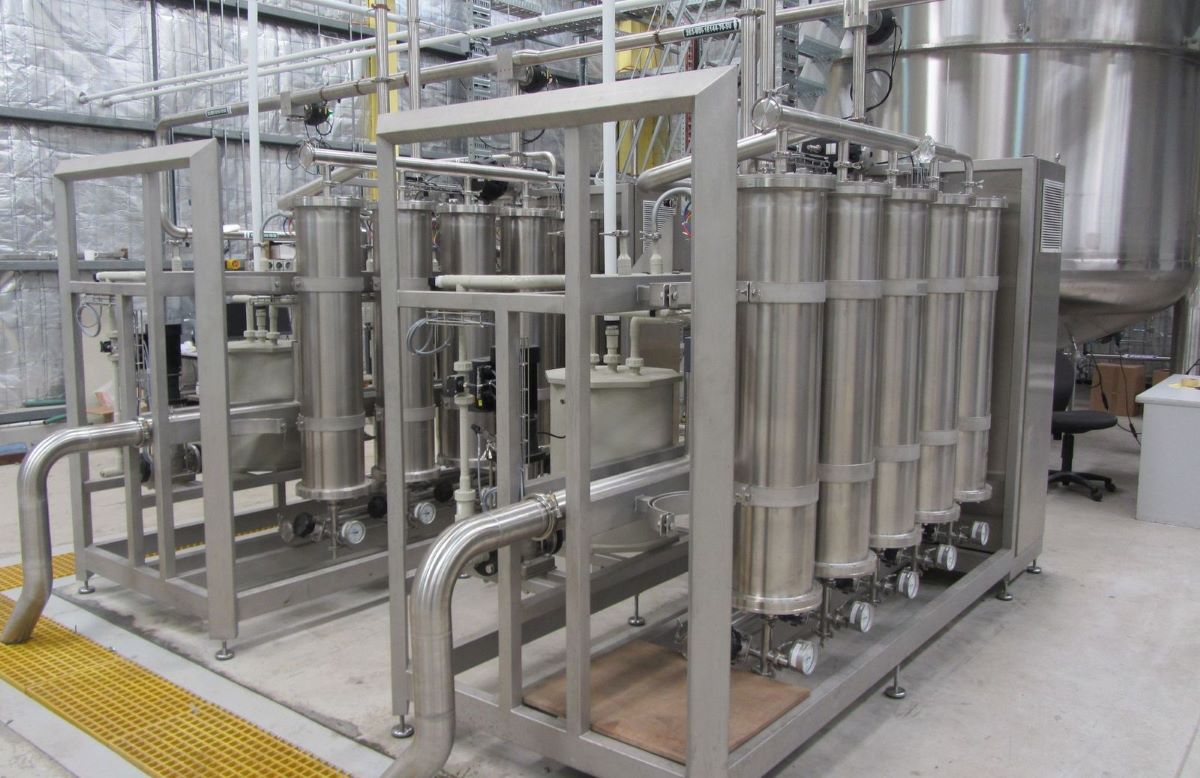
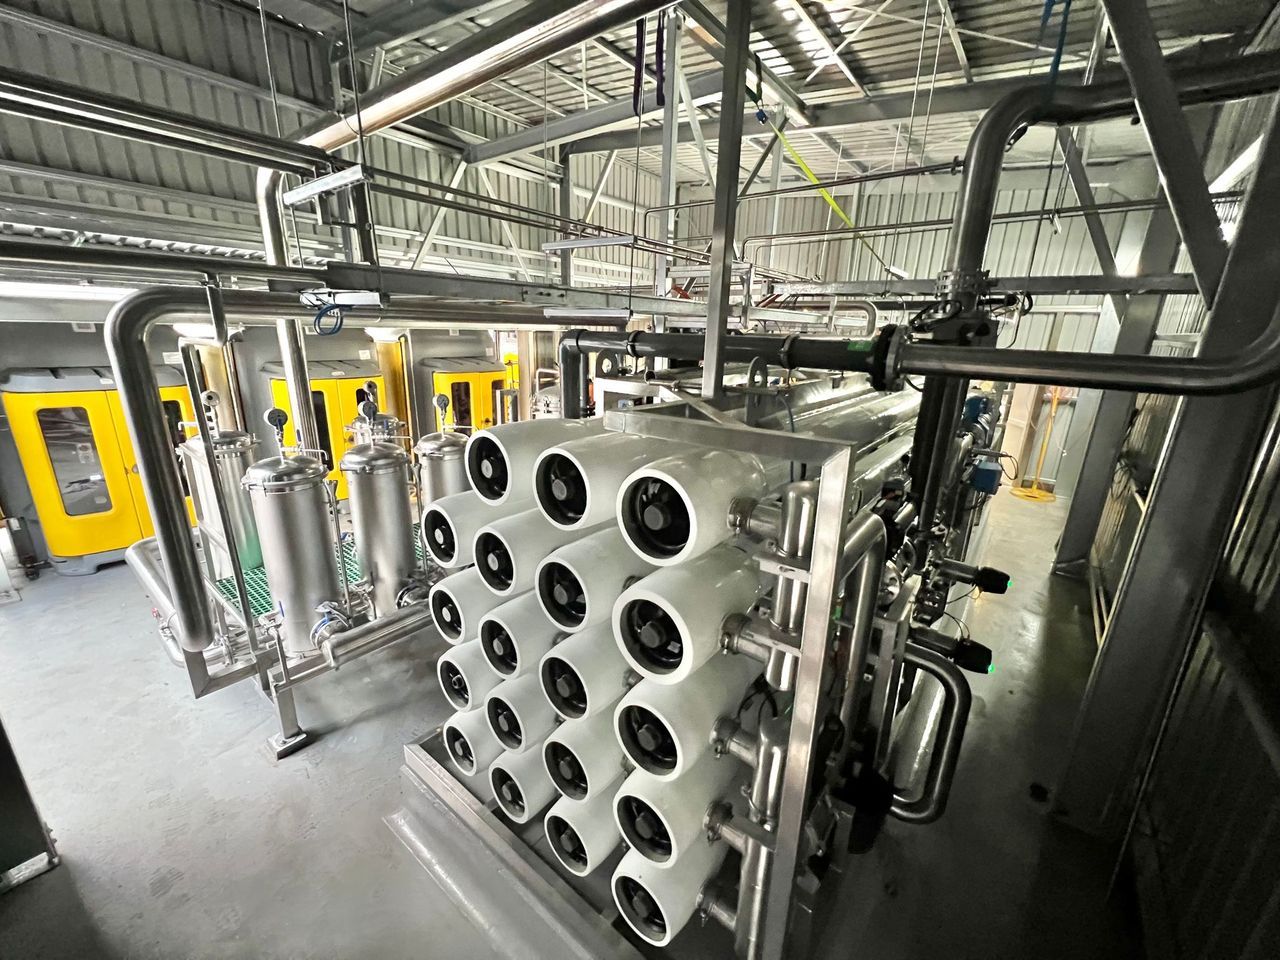
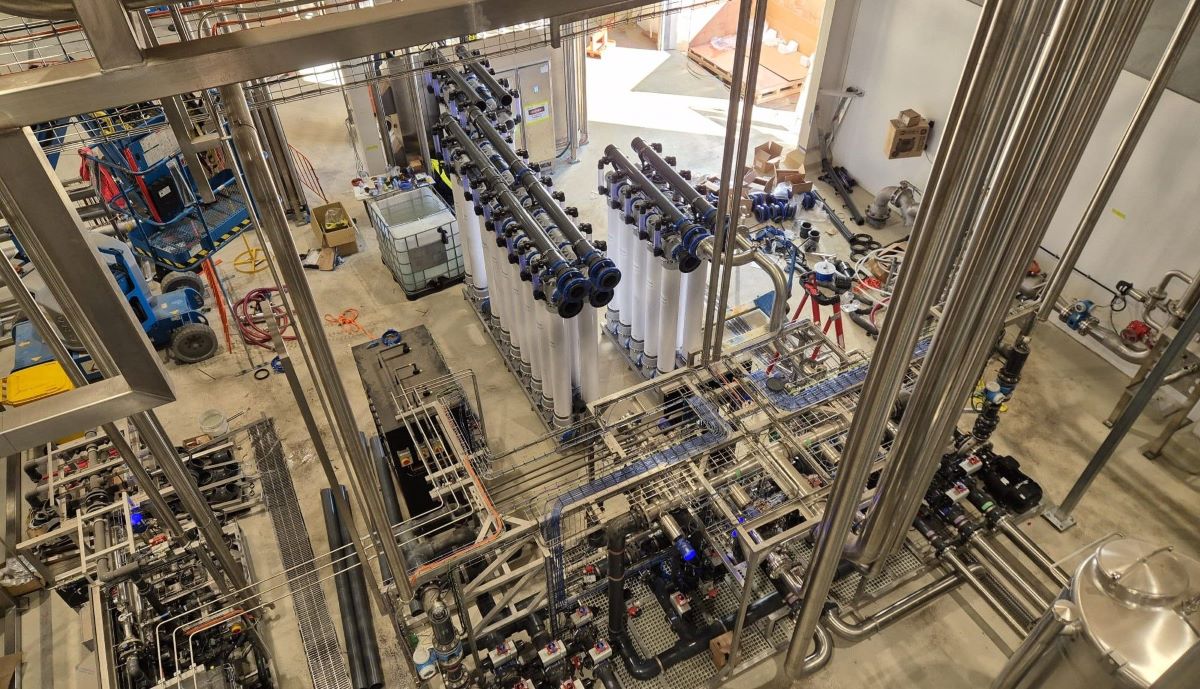
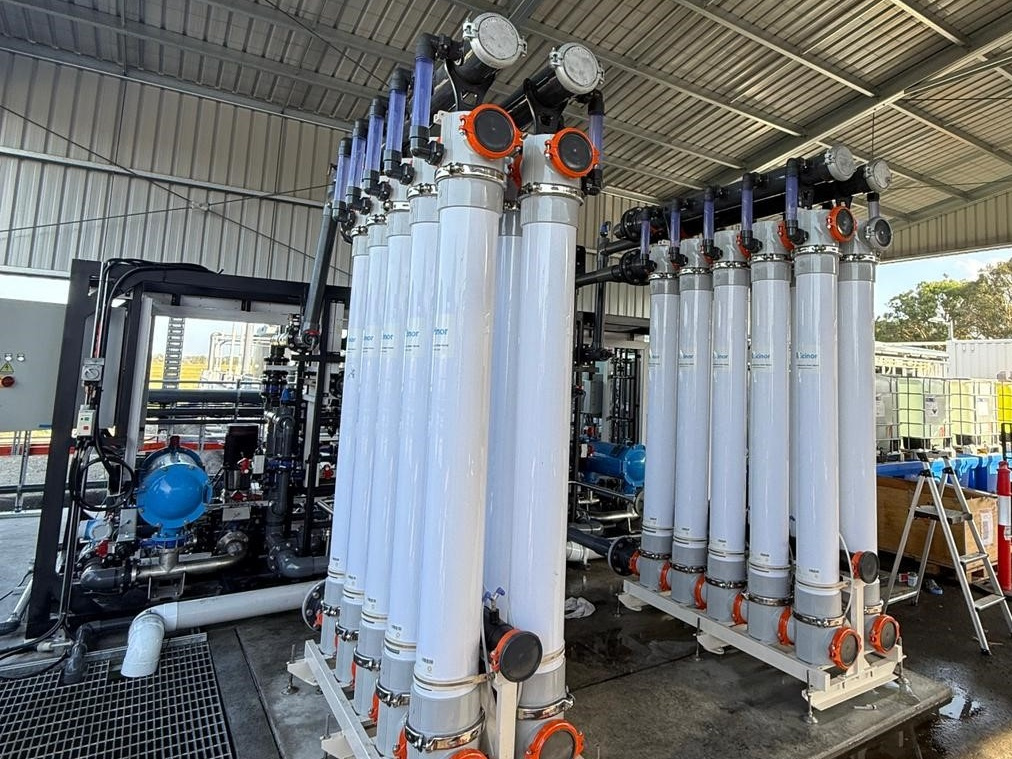
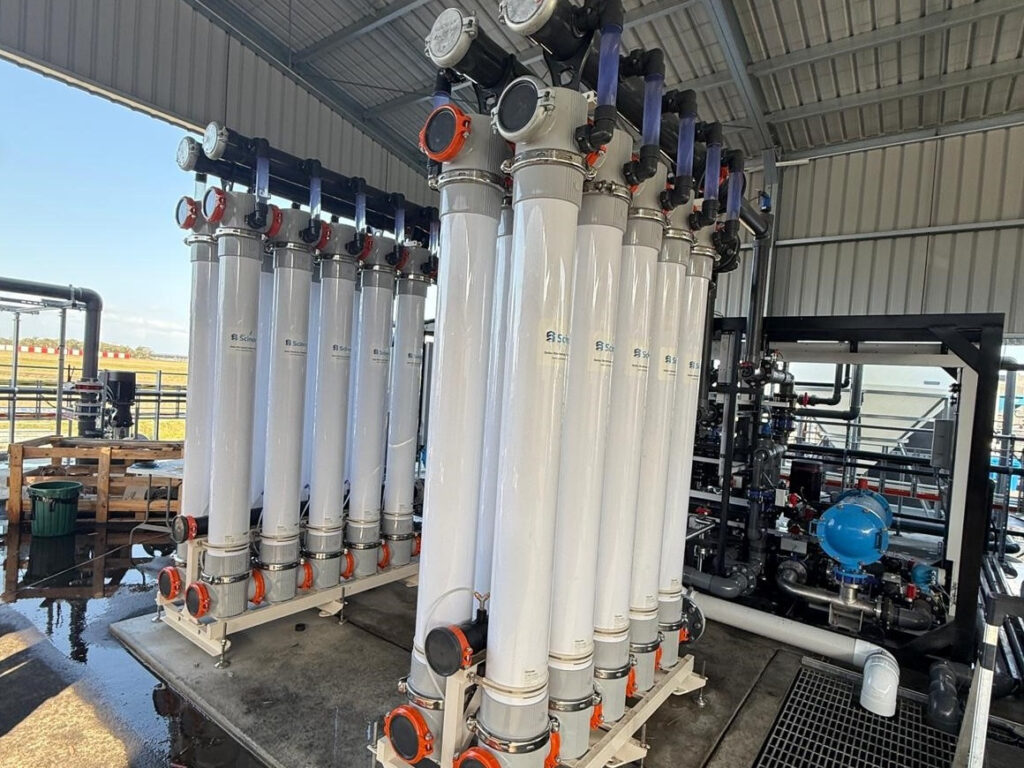
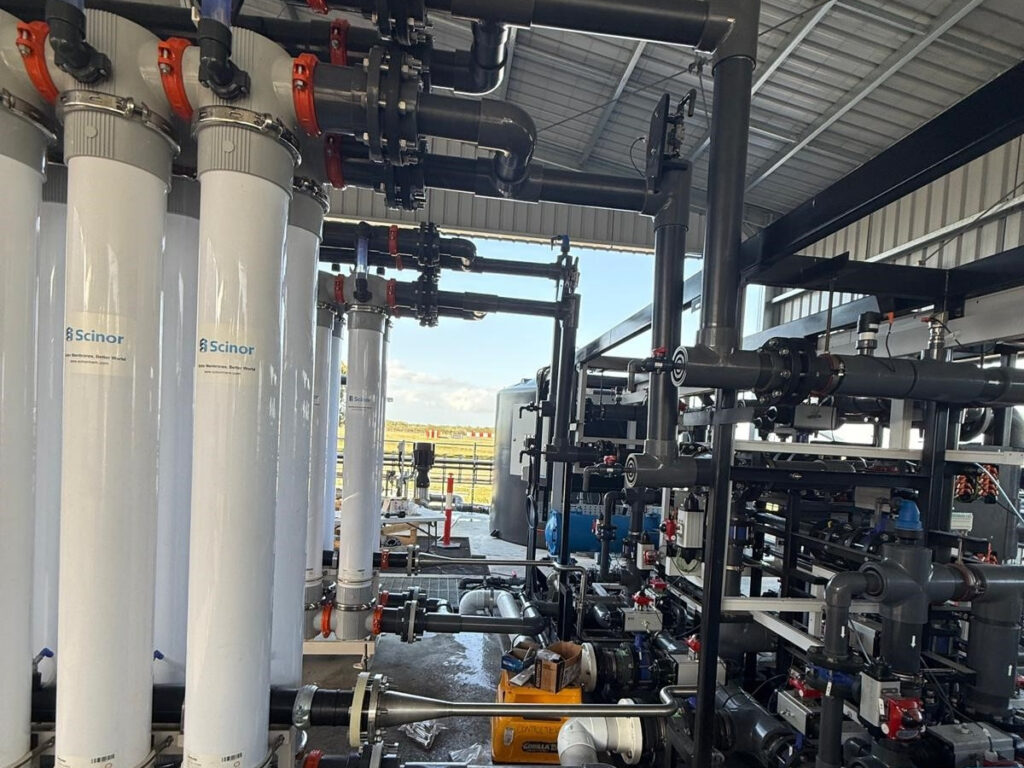
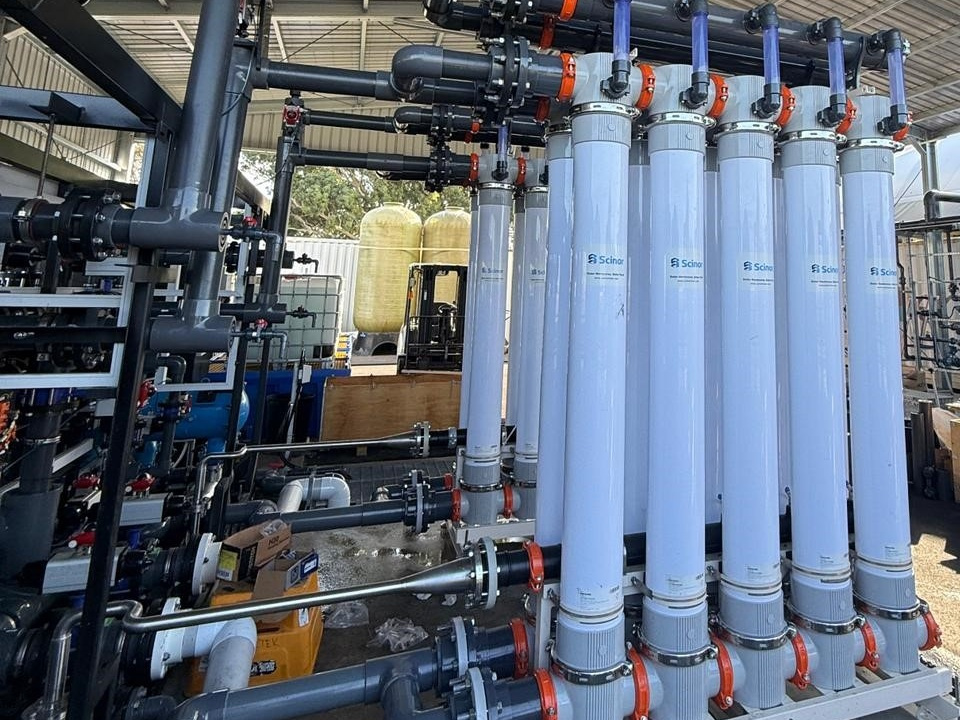
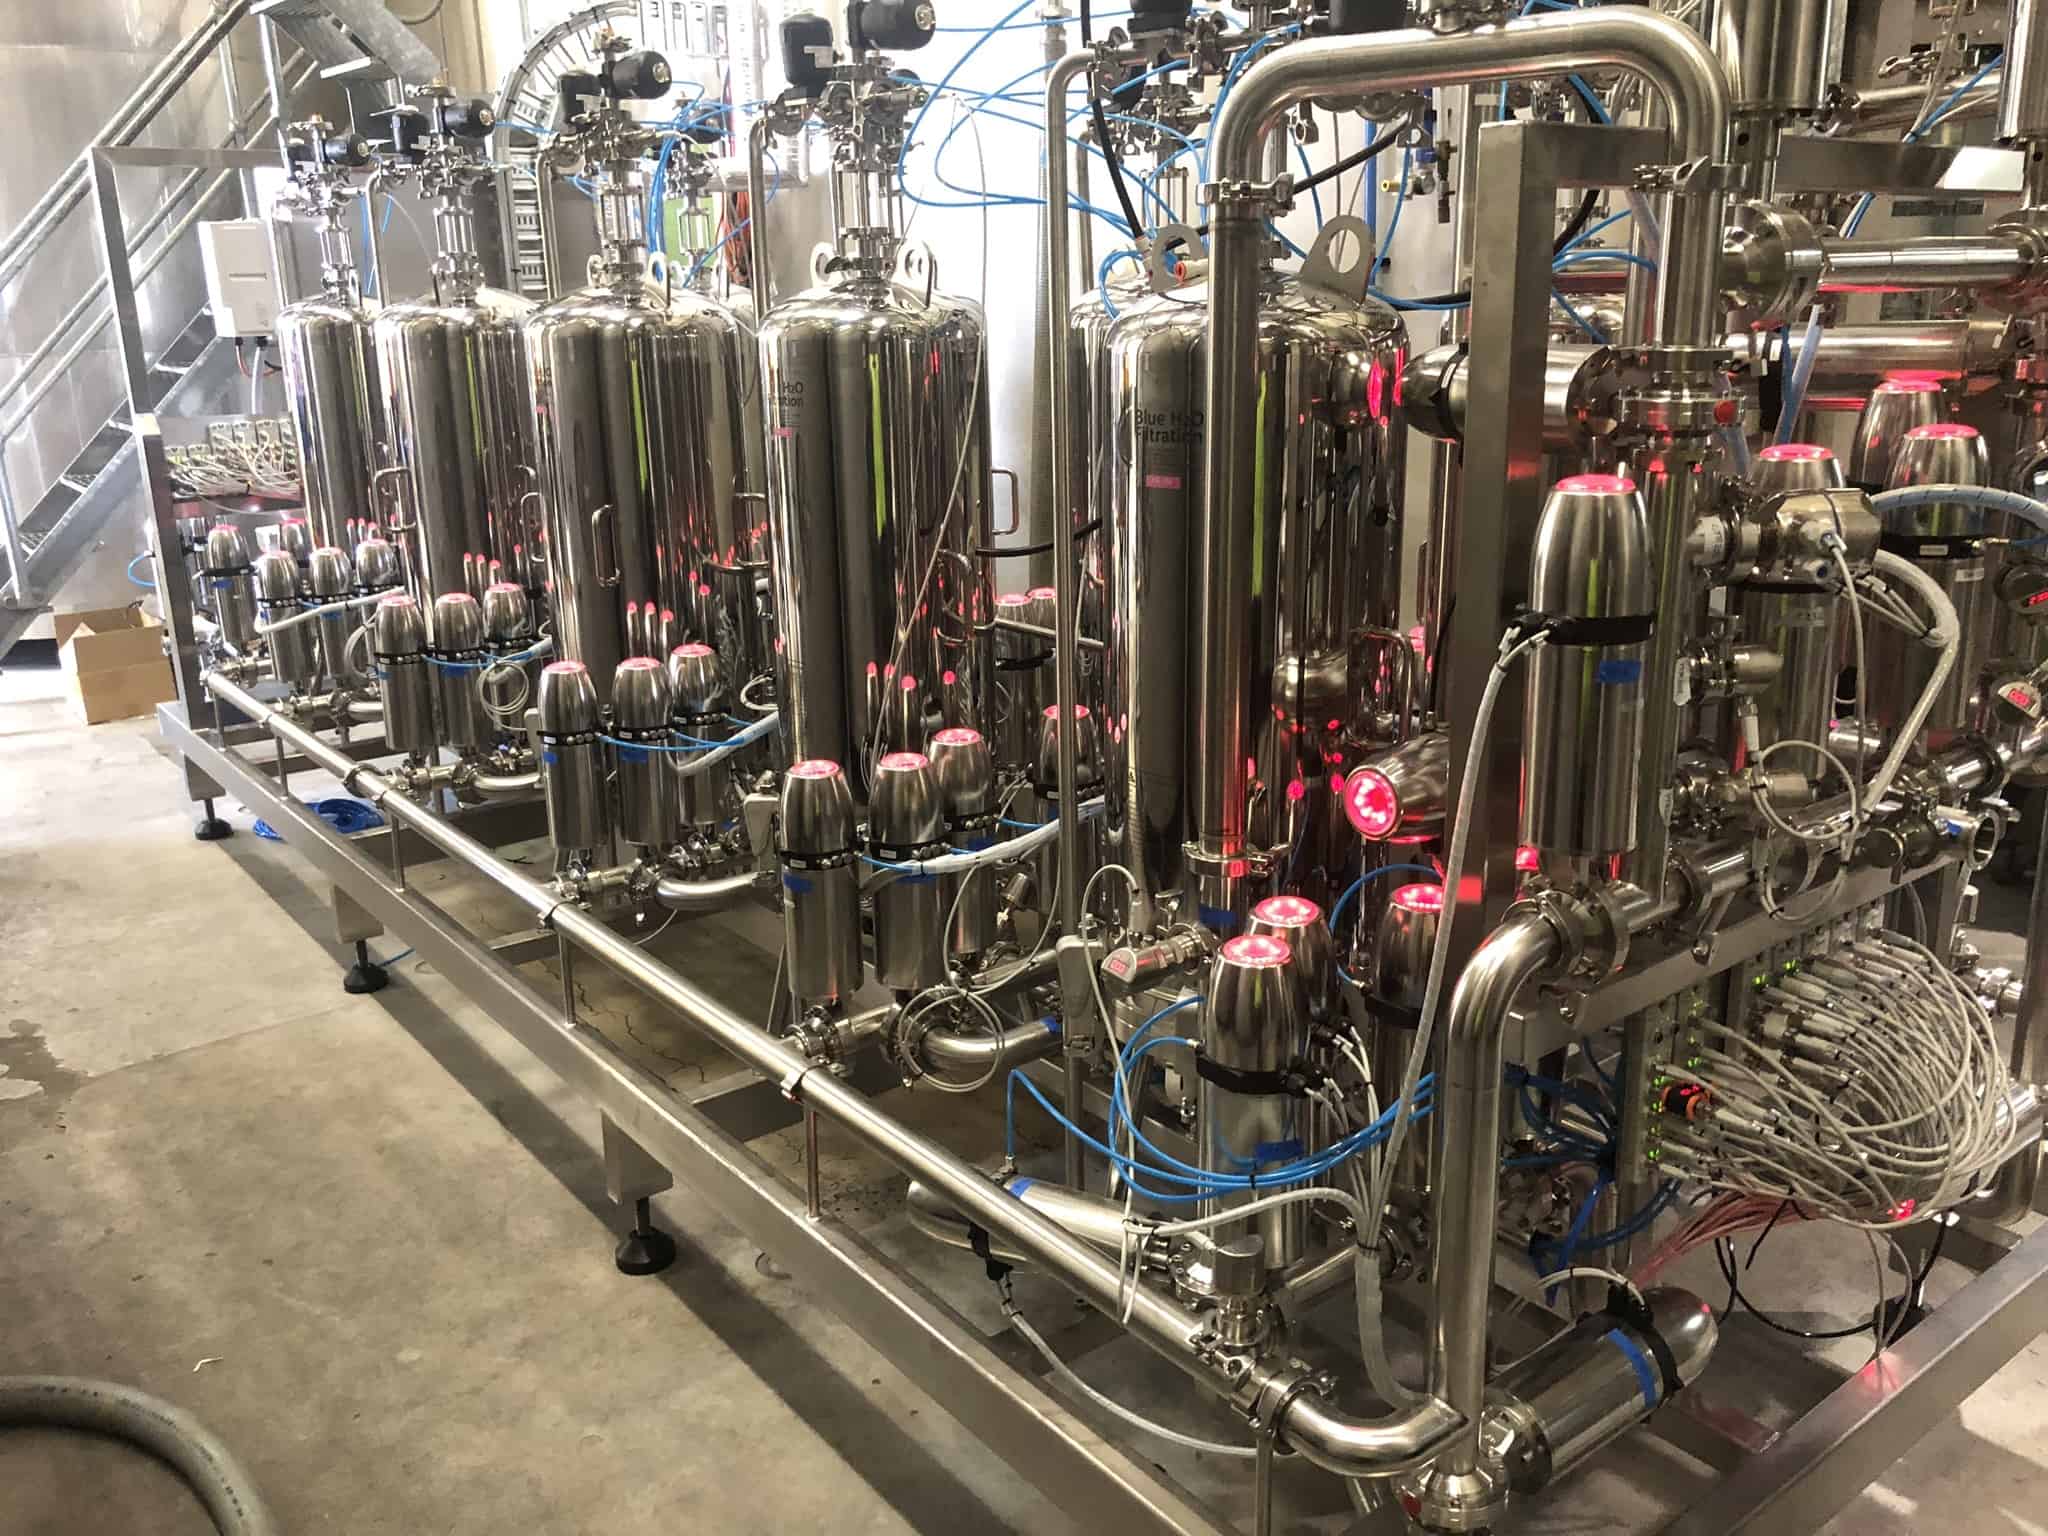
- Double-rack UF design – Two independent process trains of 10 Scinor PUFS-P80 modules each, allowing the plant to keep producing water at reduced capacity while either rack is isolated for maintenance or CIP, satisfying the site’s continuous-operation requirement.
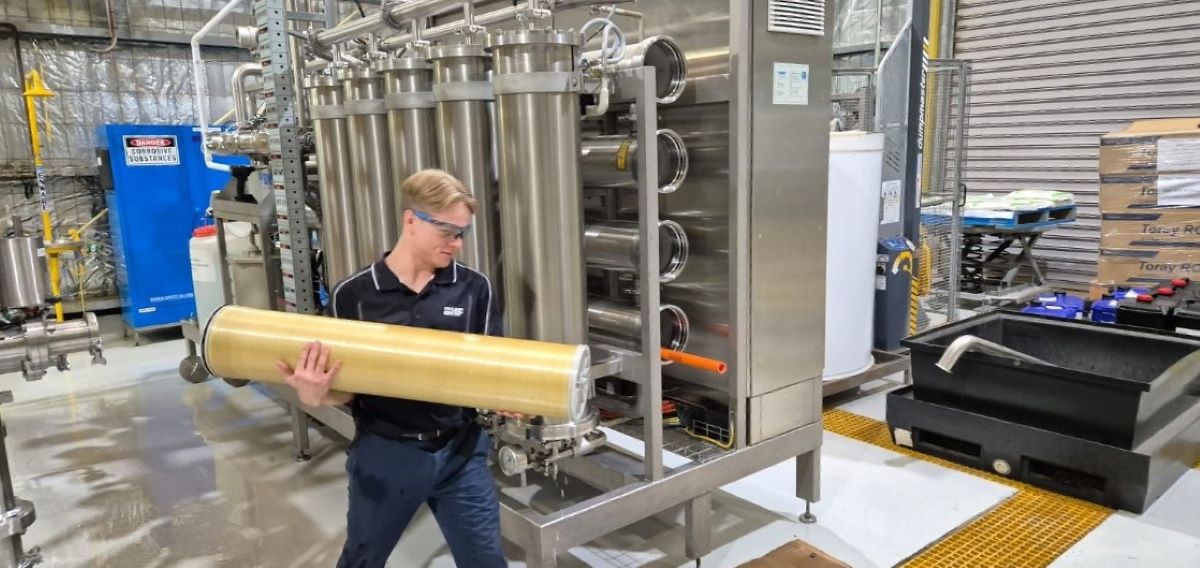
- Robust, NSF-rated membranes – Scinor’s PVDF hollow-fibre membranes, manufactured using the TIPS method, provided the mechanical strength and chemical tolerance needed to handle the site’s iron and organic loading through repeated CIP cycles, backed by a 7-year pro-rata warranty.
- Conservative flux design – Sized to an average flux of 57 LMH against a maximum permitted flux of 70 LMH, extending membrane life while retaining capacity headroom.
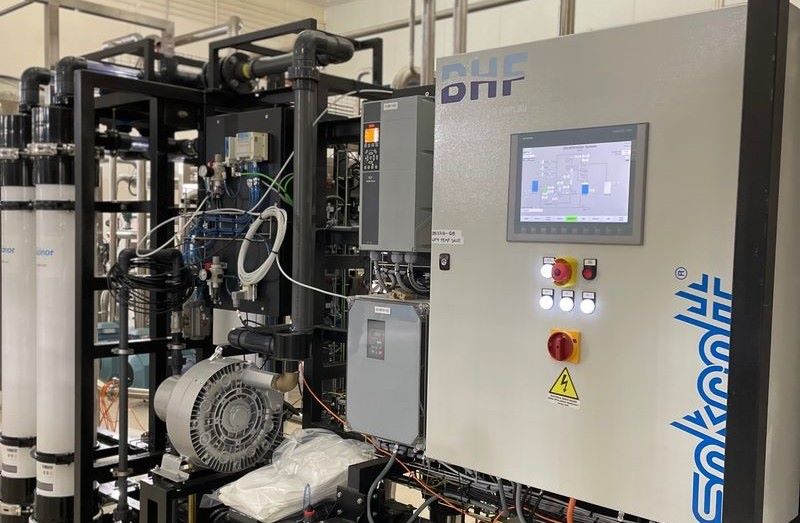
- Full automation package – An Allen Bradley CompactLogix PLC and PanelView Plus HMI running automated production, backwash (with air scour), CIP (acid, caustic and sanitise cycles), chemically enhanced backwash and automated pressure-decay integrity test sequences, plus an auto-flush feature to protect against biofilm growth during any stoppage.
- Native integration with Onterris’ control platform – The control system was configured to Onterris’ own tag mapping, numbering and Ethernet/IP conventions, giving Onterris direct visibility and control of the UF plant from its master SCADA system.
- End-to-end documentation and delivery – BHF supplied the full suite of design submittals, P&IDs, GA drawings and O&M manuals required under the tender, followed by factory acceptance testing, on-site installation supervision, commissioning, site acceptance testing and operator training.
Onterris’ UF90 system was engineered to deliver:
- Confirmed membrane integrity – Both racks passed pressure-decay integrity testing comfortably within specification immediately after module installation, confirming a leak-free system from first production.
- Fully verified commissioning – Every BHF-supplied electrical, mechanical and software function, including all production, backwash, CIP, CEB and integrity test sequences, was tested and signed off, with the plant formally declared ready for normal operation.
- Reliable, continuous pretreatment – The redundant double-rack design gives Onterris the ability to maintain production during scheduled maintenance or CIP, supporting uninterrupted operation of the wider groundwater remediation program.
- Seamless control integration – The UF control system now operates natively alongside Onterris’ Allen Bradley master platform, giving Onterris a single point of visibility and control across its treatment train.
- A protected downstream process – By consistently removing suspended solids and coagulated organics upstream, the UF system safeguards Onterris’ proprietary ion-exchange treatment system, ensuring efficient long-term PFAS remediation outcomes.
Recent Case Studies
South Taranaki District Council (STDC)
Suntory – Advancing Water Sustainability
New South Wales Brewery – Tooheys
Torresan Estate – Automated Filtration System
Want To Know More About How BHF Could Improve Your Filtration And Purification Performance?
Get in touch to find out more.